Chemicals
The chemical processing industries operate under some of the most unforgiving environments in manufacturing. Managing aggressive media, extreme thermal cycles, and high pressures requires specialized sealing technologies that mitigate risk, prevent hazardous emissions, and maximize equipment uptime.
Sealing Solutions for Chemical Industry Applications
Fluid handling and containment infrastructure, including centrifugal pumps, rotary valves, control instruments, and agitation reactors, depend on precise sealing interfaces. AST engineers high-performance sealing profiles tailored to specific chemical industry operating envelopes. Our approach integrates material science with geometry design to mitigate localized mechanical stress, fluid cross-contamination, and seal degradation within complex process loops.

Sealing Solutions for Chemical Industry Tankers
Bulk fluid transport by road, sea or rail exposes sealing components to dynamic mechanical loads. But also to thermal expansion cycles, and varied chemical payloads, including volatile hydrocarbon derivatives. AST provides high-integrity gaskets and O-rings designed to maintain constant sealing force under fluctuating torque. These components prevent atmospheric leakage and resist the corrosive profiles of diverse industrial chemical and petrochemical chemical freights during extended transport cycles.

Specialty Chemicals
The synthesis of fine and specialty chemicals often involves highly reactive reagents, specialized catalysts, and volatile solvents. Standard rubber compounds can rapidly degrade or lose structural integrity in these environments. AST addresses these severe applications with Perfluoroelastomer (FFKM) components. The chemical structure of FFKM provides near-universal chemical resistance, maintaining seal performance across highly diverse chemical matrices.
Pharmaceuticals
Sealing components within the pharmaceutical sector must provide chemical resistance while strictly adhering to regulatory standards. Materials must withstand regular Clean-in-Place (CIP) and Steam-in-Place (SIP) sterilization protocols without degrading or risking process contamination. AST supplies sealing solutions manufactured from FDA-compliant and USP Class VI certified compounds, including high-purity Polytetrafluoroethylene (PTFE) and Fluorocarbon (FKM) elastomers.
Chemical Manufacturing
Continuous bulk chemical manufacturing, including the production of polymers, synthetic rubbers, and petrochemical intermediates subjects equipment to long operational runs. Seals must resist long-term chemical attack and gas permeation to maximize the time between scheduled maintenance. AST offers targeted elastomeric selections, including FKM, Silicone, and EPDM, optimized to resist compression set and maintain elasticity over extended service lives.
Agrochemicals
Agrochemical processing involving fertilizers, concentrated acids, and complex pesticide formulations introduces both chemical corrosion and abrasive particulate slurries. Sealing systems must withstand chemical oxidation while resisting mechanical wear. AST delivers ruggedized sealing configurations utilizing hard-wearing EPDM, specialized FKM, and advanced composite materials engineered to prevent abrasion-induced leak paths.
Industry: Chemical/Medical Cleaning
The Challenge
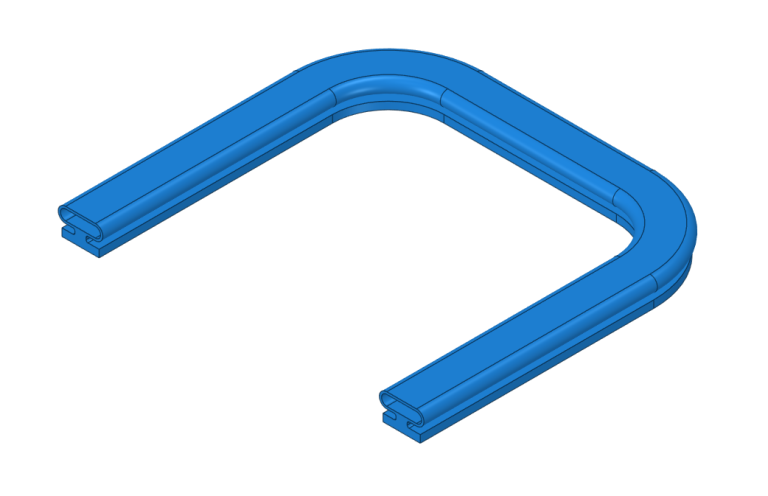
SIP systems in medical equipment processing expose sealing components to a tough combination of high temperatures, pressure, and aggressive sterilization chemicals. Preventing chemical steam from leaking into surrounding work areas is critical for safety and process integrity.
Our Solution
We engineered a custom inflatable SIP seal moulded from a smooth, high-grade elastomer specifically chosen for severe chemical and thermal resistance. When inflated, the seal expands uniformly to create an airtight, press-fit barrier that safely holds back hot chemical vapors during active sterilization.
Why Choose AST for Your Chemical Sealing Needs?
At AST, we understand the unique challenges of sealing applications in the chemical industry. With over 40 years of experience in the sealing industry, we have developed a reputation for providing high-quality and reliable sealing solutions. Our team of sealing experts works closely with customers to understand their specific needs and provide customized sealing solutions that maximize performance, durability, and safety. From FDA-approved materials to custom-engineered designs, we have the knowledge and expertise to help our customers achieve their sealing objectives. Choose AST for your chemical sealing needs and experience the difference of working with a trusted partner in the sealing industry.
