Water Management
Advanced Sealing Technology delivers high-performance sealing systems engineered for demanding water treatment and wastewater environments. From filtration systems to pumping stations and chemical dosing units, our solutions ensure long-term reliability, chemical resistance, and leakage control.
Advanced Sealing Performance for Demanding Water Systems
Water and wastewater systems operate under continuous exposure to pressure fluctuations, aggressive media, and strict environmental compliance requirements. Seal failure in these systems can result in contamination risk, downtime, and costly maintenance.
Advanced Sealing Technology develops sealing solutions specifically engineered for:
- Continuous immersion in water and effluents
- Exposure to chlorine, acids, alkalis, and cleaning agents
- High-cycle mechanical movement in pumps and valves
- Long service intervals with minimal maintenance
Our focus is simple, we aim to maximize system reliability through engineered sealing performance
Engineered for Water Applications
Every water management system has its own operational requirements. Factors such as pressure, temperature, and mechanical movement all influence sealing performance. Selecting the right material and seal design is therefore essential to ensuring reliability.
Our sealing solutions are developed to support a wide range of water-related applications, including pumping systems, control valves, filtration equipment, membrane installations, treatment units, and pipeline networks. By focusing on the specific operating conditions of each application, we provide sealing solutions that deliver consistent performance while reducing maintenance demands.
Rather than relying on generic products, we work closely with customers to identify the most effective sealing solution for their system requirements.
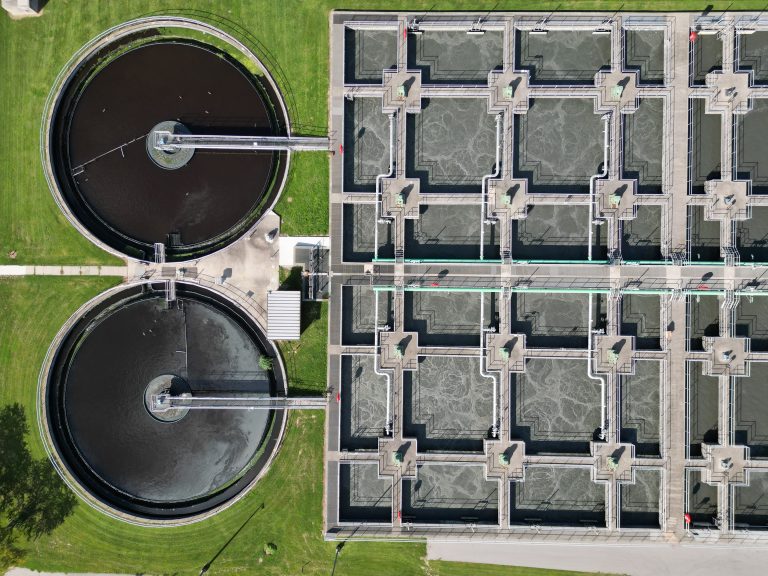
Industry: Water and Waste Management
The Challenge
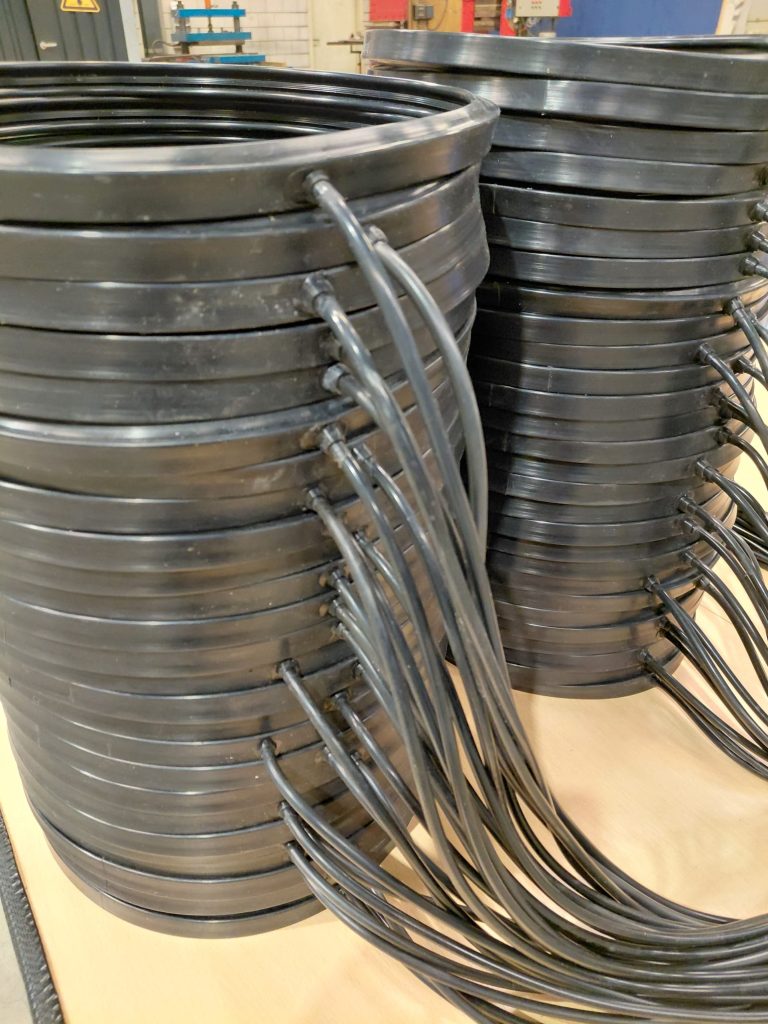
The customer was looking for a new solution for a water treatment system due to the presence of drugs and pharmaceutical residues in the water. In this case, the sealing surfaces were uneven, so a standard solution was not sufficient.
Our Solution
We created custom inflatable seals which were capable to support the uneven sealing surfaces for the system, based on the information the customer supplied. These seals were then tested and approved by the customer for its compatibility with the system.
Material Selection for Water Management Applications
Selecting the right sealing material is essential for ensuring long-term performance in water management systems. Factors such as chemical exposure, operating temperature, pressure, and mechanical movement all influence material suitability. Below are some of the most commonly used sealing materials in water infrastructure and their typical applications.
EPDM
EPDM is one of the most widely used sealing materials in water management applications due to its excellent resistance to water, steam, weathering, and UV exposure.
NBR
NBR, also known as Nitrile Rubber, offers a strong balance between mechanical performance and cost-effectiveness. It provides good resistance to wear and performs well in applications where water may be present alongside oils, lubricants, or hydraulic fluids.
FKM
FKM is a high-performance sealing material known for its excellent resistance to chemicals, elevated temperatures, and harsh operating environments.
PTFE
PTFE is valued for its exceptional chemical resistance and is often selected for applications involving treatment chemicals or aggressive cleaning agents. Its low-friction properties also make it suitable for dynamic sealing applications where smooth movement and reduced wear are important.
Polyurethane (PU)
Polyurethane is widely recognised for its outstanding wear resistance and mechanical strength. These characteristics make it particularly suitable for applications where seals are exposed to continuous movement, pressure fluctuations, or abrasive conditions.
Partner with Advanced Sealing Technology
Reliable water management depends on reliable sealing technology. With extensive expertise in materials, applications, and engineering support, Advanced Sealing Technology helps organisations improve system performance while reducing operational risk.
Whether you are designing new infrastructure, upgrading existing equipment, or addressing a specific sealing challenge, our experts are ready to support your project with practical advice and application-focused solutions.
Contact our team of experts to discuss your water management application.